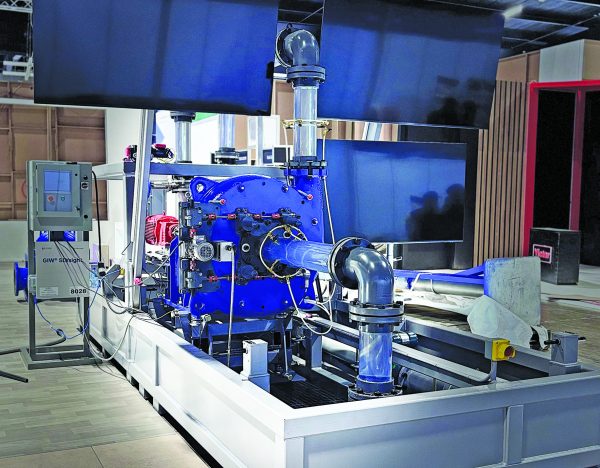

KSB Pumps and Valves hosted a unique live display of its latest slurry pump technology at Electra Mining Africa 2026, featuring a fully monitored and adjustable MDX pump circuit that operated at regular intervals throughout the event.
The demonstration showed how advanced monitoring and adjustment technologies can transform the way slurry pumps are operated and maintained using a live GIW MDX with KSB’s proprietary SLYsight and RAMSL technology that provides the operator with live monitoring data and the ability to set the pump’s liner parameters for optimum performance in the space of minutes, rather than hours it would take to perform the same setting on traditional slurry pumps.
According to KSB Pumps and Valves market area manager for mining, Jacques Pretorius, the heavyweight unit was brought to
South Africa from GIW’s operation in Grovetown, USA, in two 20-foot containers and operated using water containing small urethane cylinders to simulate slurry characteristics. This allowed visitors to see the pump operating through the transparent piping and hear the particles moving through the pump, while also viewing live data as the settings changed.
“We wanted to demonstrate to the sub-Saharan African mining industry what technology can achieve, how it can improve performance, as well as how it can prolong the lifespan and extend service intervals of pumps in the field. It was the first time that we showed our MDX slurry pump using RAMSL technology which enables quick adjustment of the suction liner to maintain the optimum clearance or ‘nose gap’ between the stationary liner and rotating impeller.
“This is critical to slurry pump performance, as wear can change the gap between it and the impeller as it increases, which allows slurry to recirculate around the front of the impeller instead of moving efficiently through the pump. The result is usually reduced hydraulic efficiency and premature component failure.
“Slurry pumps operate in some of the most demanding environments in the minerals processing chain with abrasive and often highly variable slurries continuously attacking internal components, so wear is inevitable.
The challenge is to understand it, manage it and intervene before it develops into an unplanned failure,” says Pretorius.
He explains that KSB’s RAMSL technology provides an automated way of managing this critical clearance rather than a maintenance team having to undertake lengthy manual adjustments. Visitors could see the liner being moved towards the rotating impeller before the system brought the liner into contact with it and backed it off to establish the required nose gap. The adjustment can be made in small increments, allowing the pump to be set accurately for optimum operation.
“It takes people out of harm’s way and makes the adjustment much quicker and simpler.”
Pretorius continues that SLYsight complements RAMSL with its sensor-based monitoring technology which is designed to provide wear data on the inside of the slurry pump where various sensors monitor wear and other critical parameters at different points within the pump. The data can then be monitored to check the wear condition and monitor changes over time. This gives the operators a clear indication of the internal condition of the pump rather than waiting for regular inspections as is usually the case.
Keith Hedges, KSB Pumps and Valves sales manager for valves, says the largescale MDX display was complemented with the equally impressive KSB DN600 knife gate valve with pneumatic cylinder and a DN400 pinch valve which weighs approximately 500 kg and 300kg respectively. In slurry applications KSB’s valve solutions provide precise and reliable flow controls to prevent damage and wear to expensive pipeline infrastructure and for reliable operation in tough slurry conditions.